Load & assemble
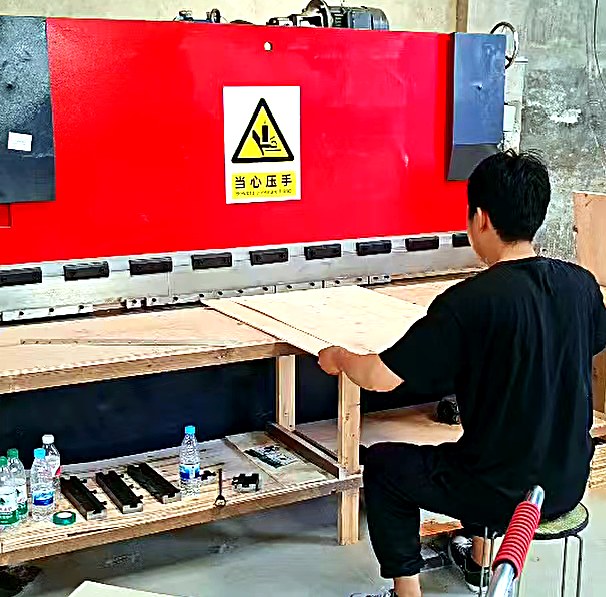
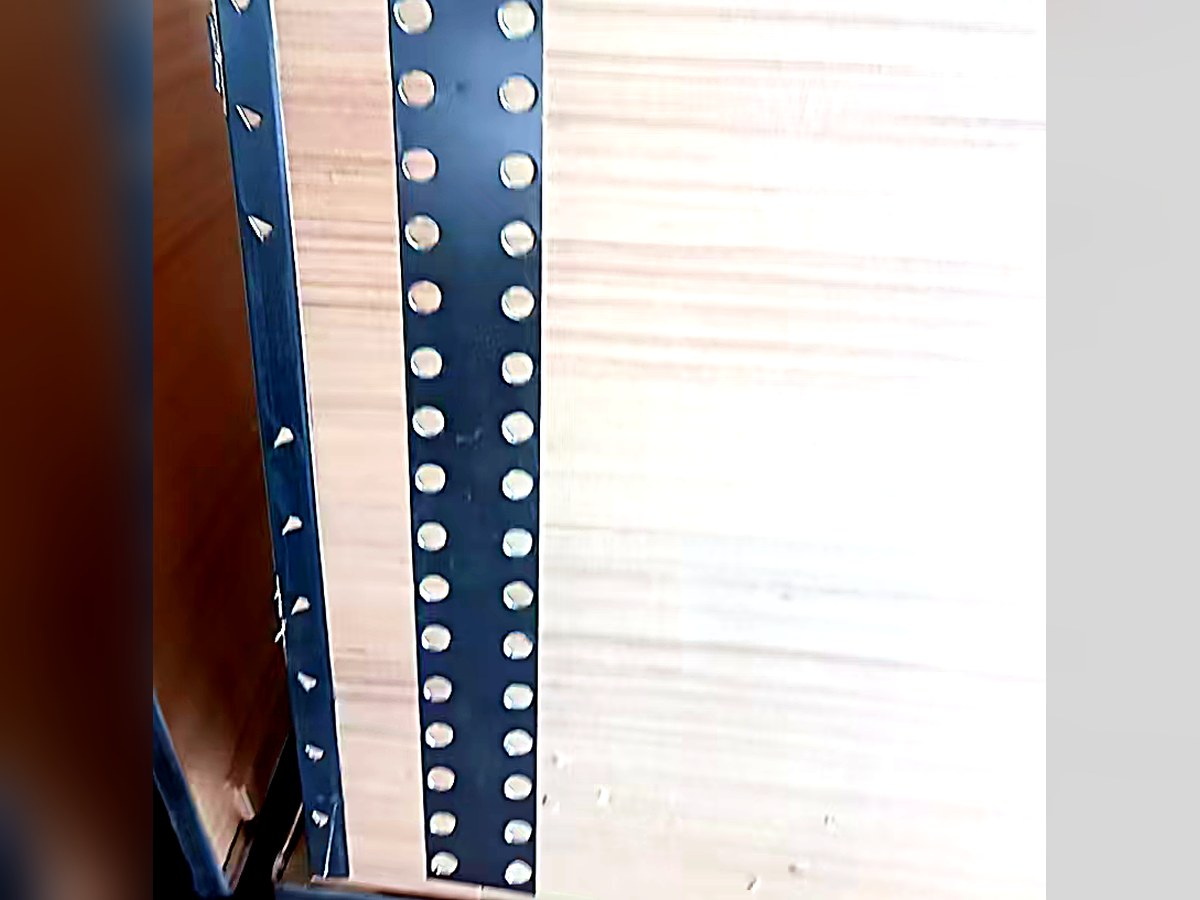
Place the steel edge and prepared plywood on the worktable.
Applies stable hydraulic force to join preformed steel edges with plywood, creating flat, rigid and dimensionally consistent box panels.
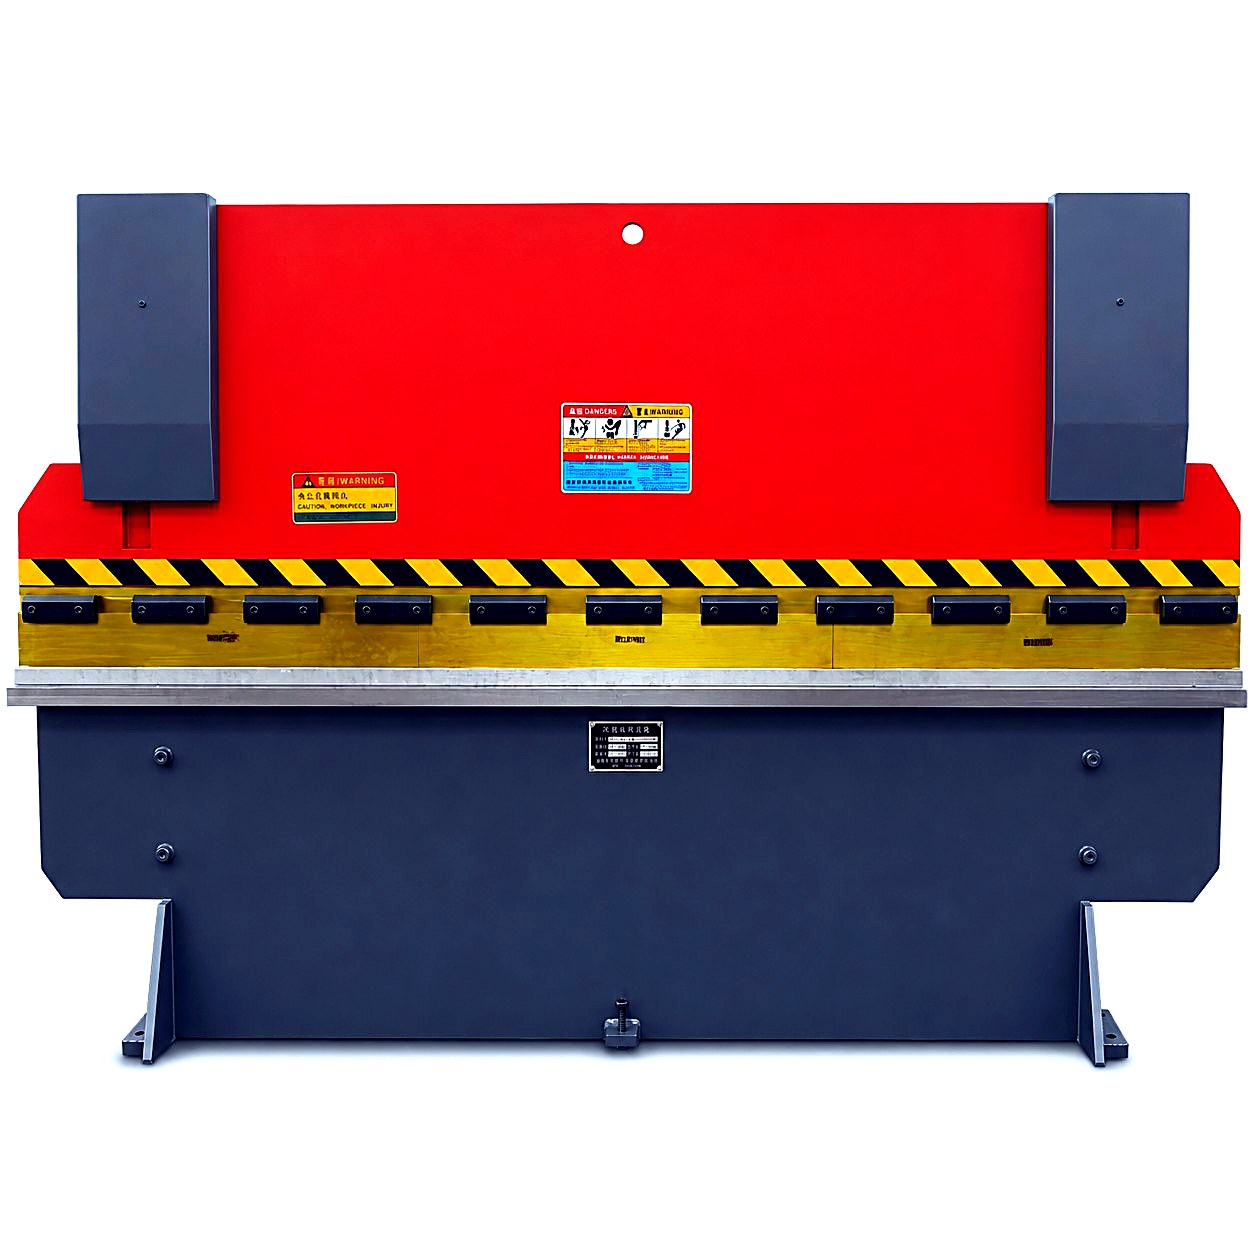
The YA2500 hydraulic press completes the steel-edged panel: it applies stable, uniform force to join preformed steel edges with prepared plywood, producing flat, rigid panels with consistent dimensions. Magnetic dies slide out for fast removal and changeover. The YA series covers three working widths — YA1600 (1.6 m, 30 tons), YA2500 (2.5 m, 30 tons) and YA3200 (3.2 m, 60 tons) — so the press matches the box size instead of forcing one frame to do everything.
Uniform pressure ensures tight, repeatable assembly
Magnetic quick-change dies slide out for fast changeovers
Light curtains, emergency stops and overload protection
Three working widths (1.6 / 2.5 / 3.2 m) match the press to the box size
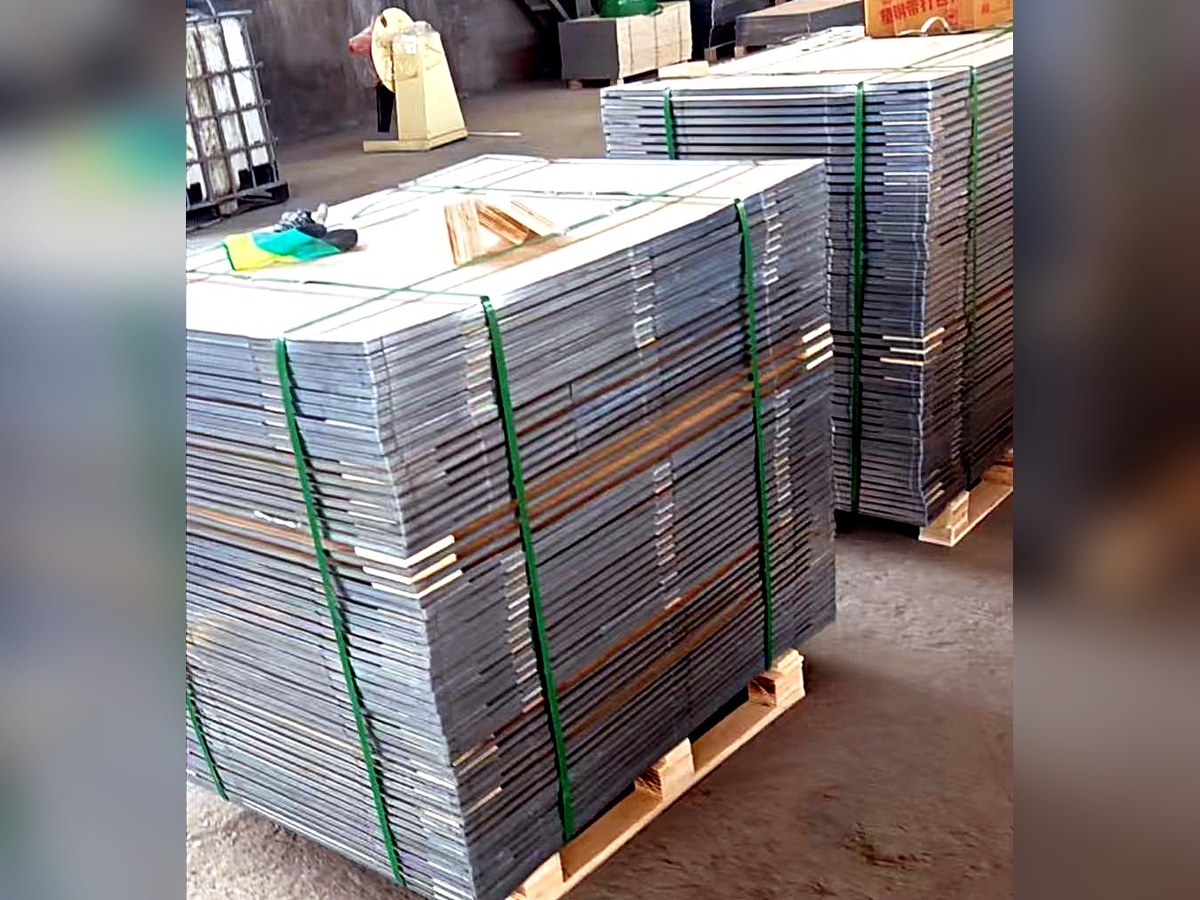
Steel-edged plywood box panels
Large export packaging cases
Heavy-duty machinery crates
Custom oversized box production
Standard configuration data. Machines are configured to order — contact us for values matched to your product.
| Model | YA2500 |
|---|---|
| Working width | 2.5 m |
| Nominal pressure | 30 tons |
| Motor power | 3 kW |
| Machine weight | 1.5 tons |
| Machine size (L×W×H) | 2,500 × 950 × 1,900 mm |
| Die system | Magnetic dies, sliding quick-change |
| Recommended working area | 3 × 3 m |
Available variants: YA1600 — 1.6 m working width, 30 tons nominal pressure; YA3200 — 3.2 m working width, 60 tons nominal pressure.
Place the steel edge and prepared plywood on the worktable.
Mechanical stops align components and control assembly gaps.
The platen descends evenly and applies the specified pressure.
After a short hold, the platen returns automatically, ready for the next panel.
Check the hydraulic oil level, lines and joints for leaks, dies and press plates for cracks, and the e-stop and wiring. Jog the cylinder up and down empty to confirm smooth travel.
Set the pressure valve to the value for the strip and panel thickness, and adjust the travel limit so the ram cannot over-press the strip or panel.
Lay the steel edge or panel to be pressed flat and centered on the die, aligned and stable.
Step on the foot switch (or press both start buttons): the ram descends slowly and presses the strip into shape. Hold pressure 1–3 seconds, then release — the ram returns automatically.
Remove the finished piece, place the next workpiece, and repeat. Never overload the press or exceed the rated stroke.
Return the ram to its top position, switch off the motor and main power. Clean iron filings and oil from the table and wipe the machine down.
Safety: keep hands, arms and head out of the ram zone during pressing. Stop immediately on oil leaks, unusual noise, low pressure or electrical faults — never run a faulty machine.