Strip feeding
Guides align the coiled strip for stable, continuous delivery.
Cold-rolls coiled steel strip into accurate steel-edge profiles for plywood box frames, with encoder cut-to-length and touchscreen control.
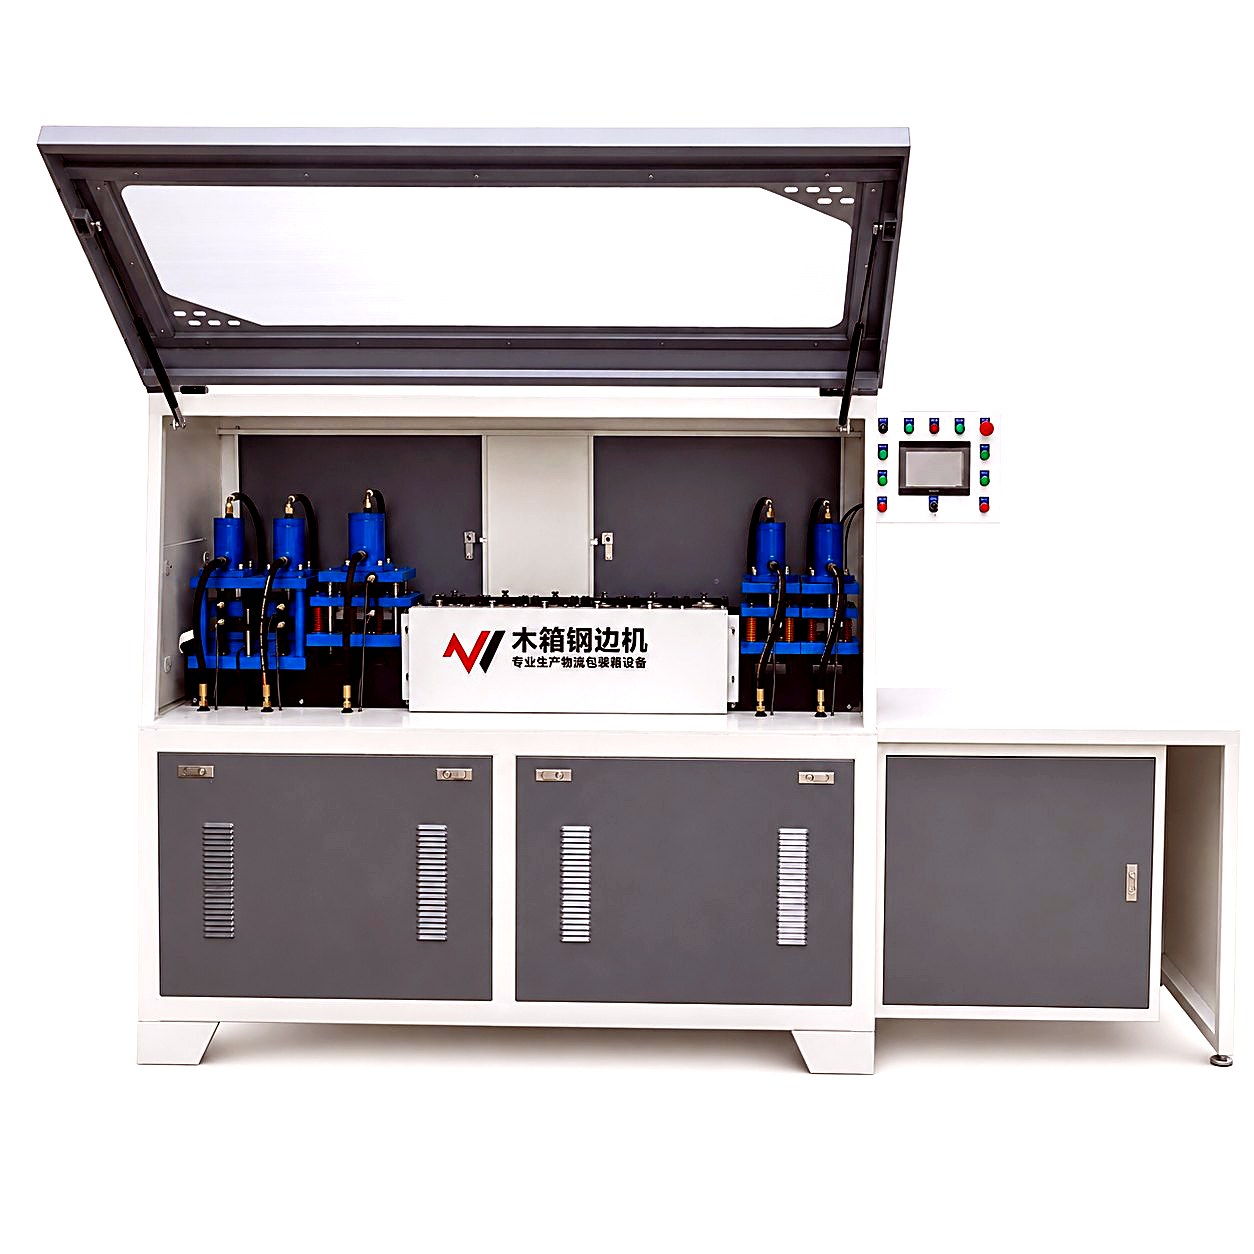
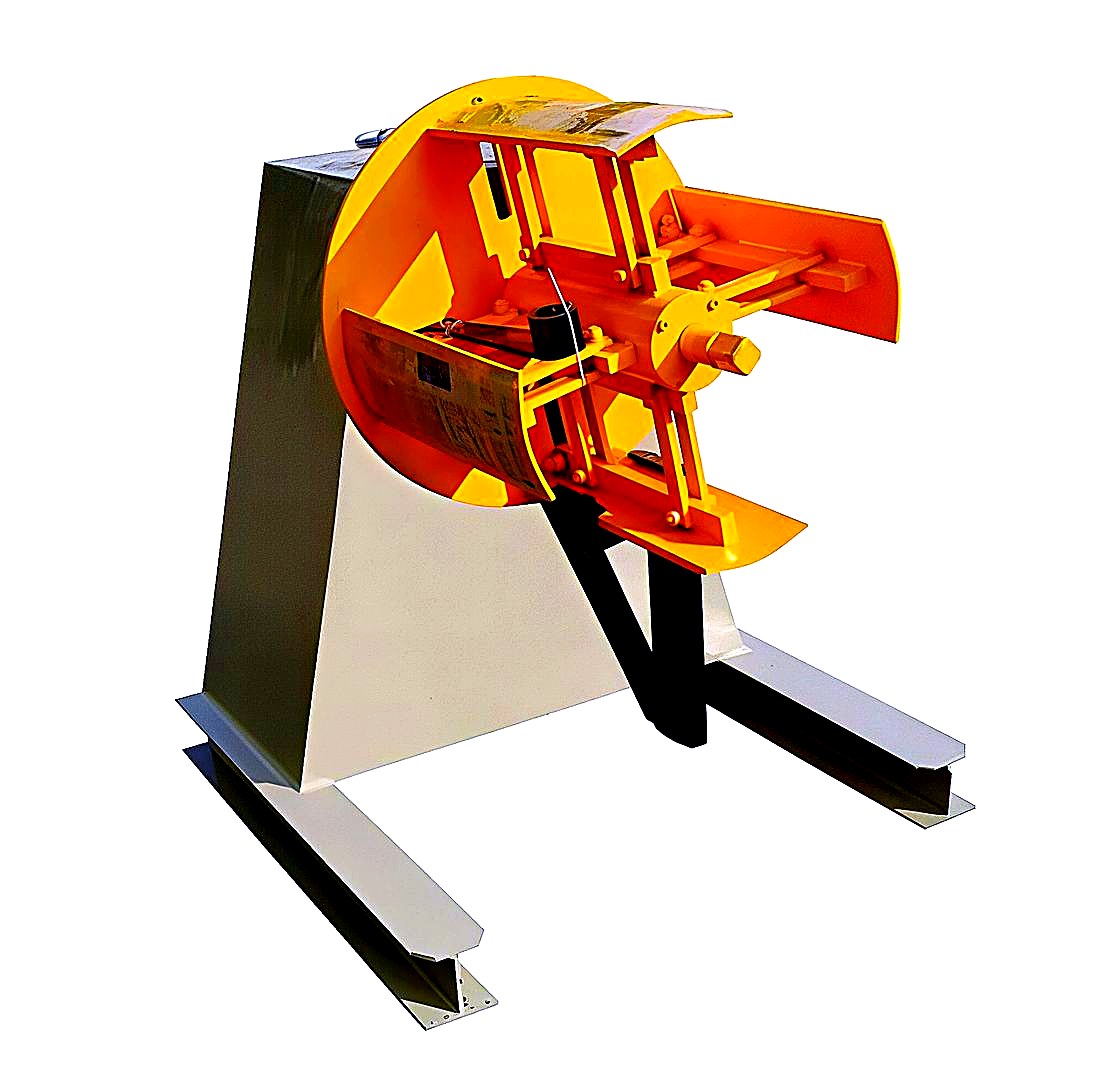
The GA-8000 cold-rolls coiled steel strip into the edge profiles that frame and reinforce nailless plywood boxes. Multi-stage rollers produce smooth, consistent profiles, an Omron PLC with Inovance servo drive synchronizes feeding and forming, and the encoder measures and cuts each profile to the preset length automatically. Modular tooling adapts the machine to different profiles with quick changeovers. An automatic steel strip decoiler is included as standard, and a dual-output configuration is available for two strip profiles from one machine.
Multi-stage rollers produce smooth, consistent profiles
Synchronized servo feeding supports stable continuous output
Modular tooling adapts to different profiles with quick changeover
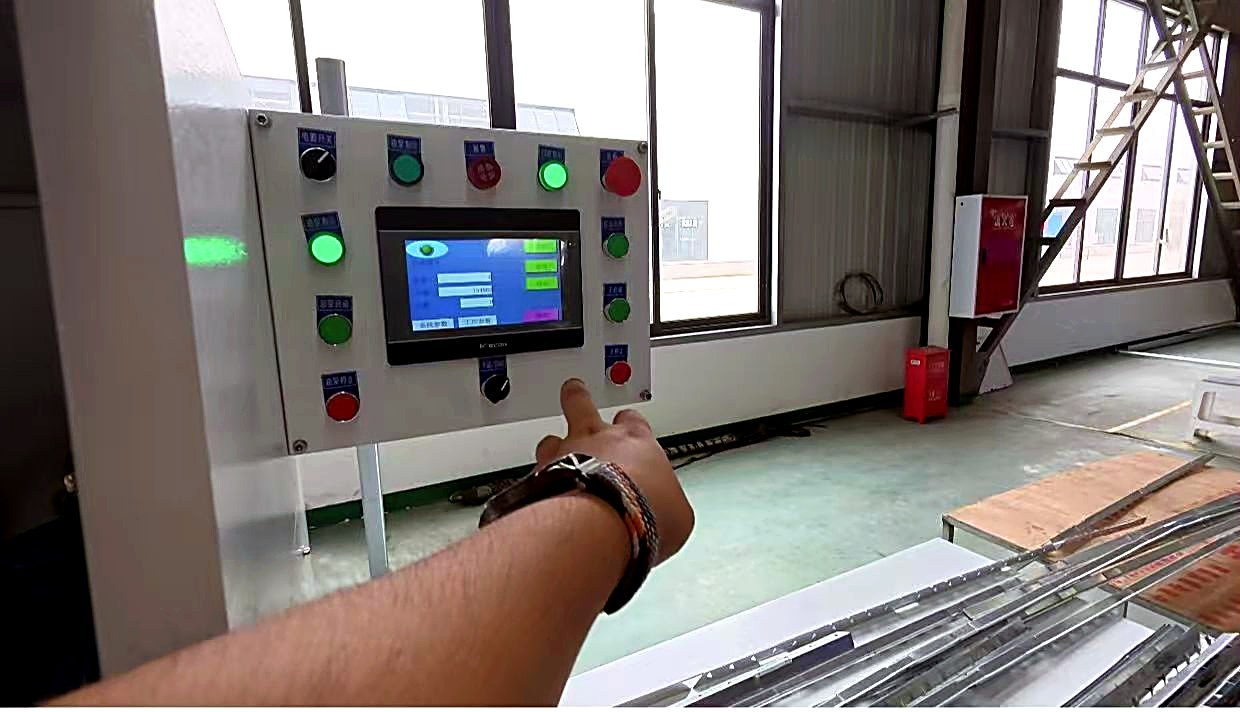
Touchscreen control with visual settings and fault prompts
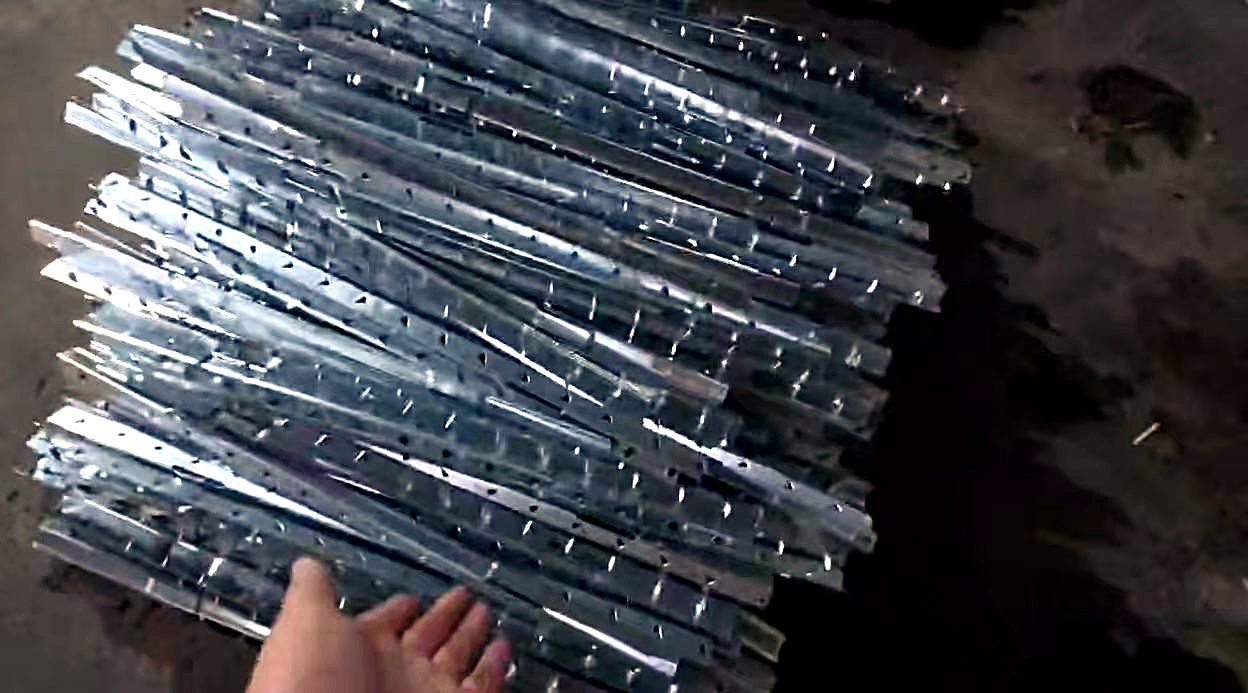
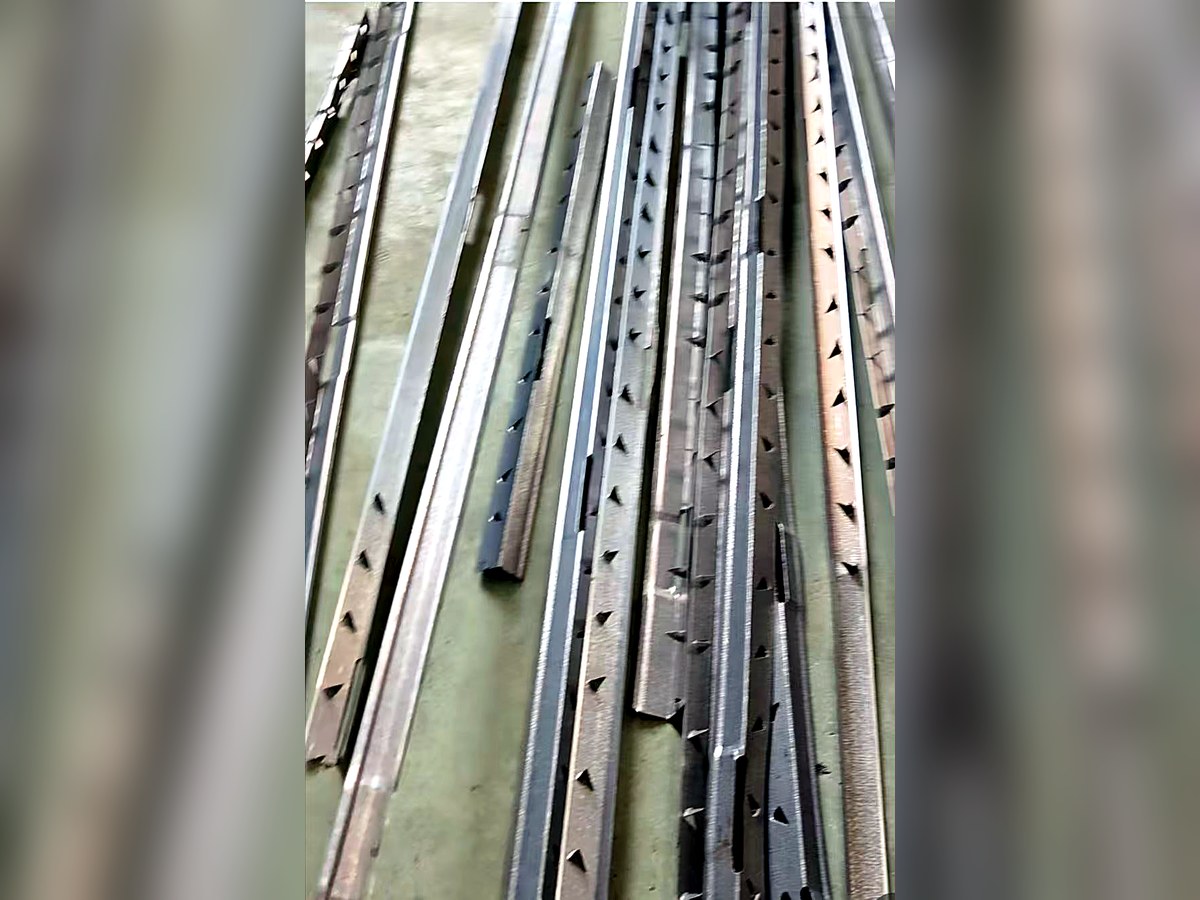
Steel-edge profiles for plywood boxes
Box frame reinforcement strips
Collapsible box connecting strips
Custom roll-formed steel components
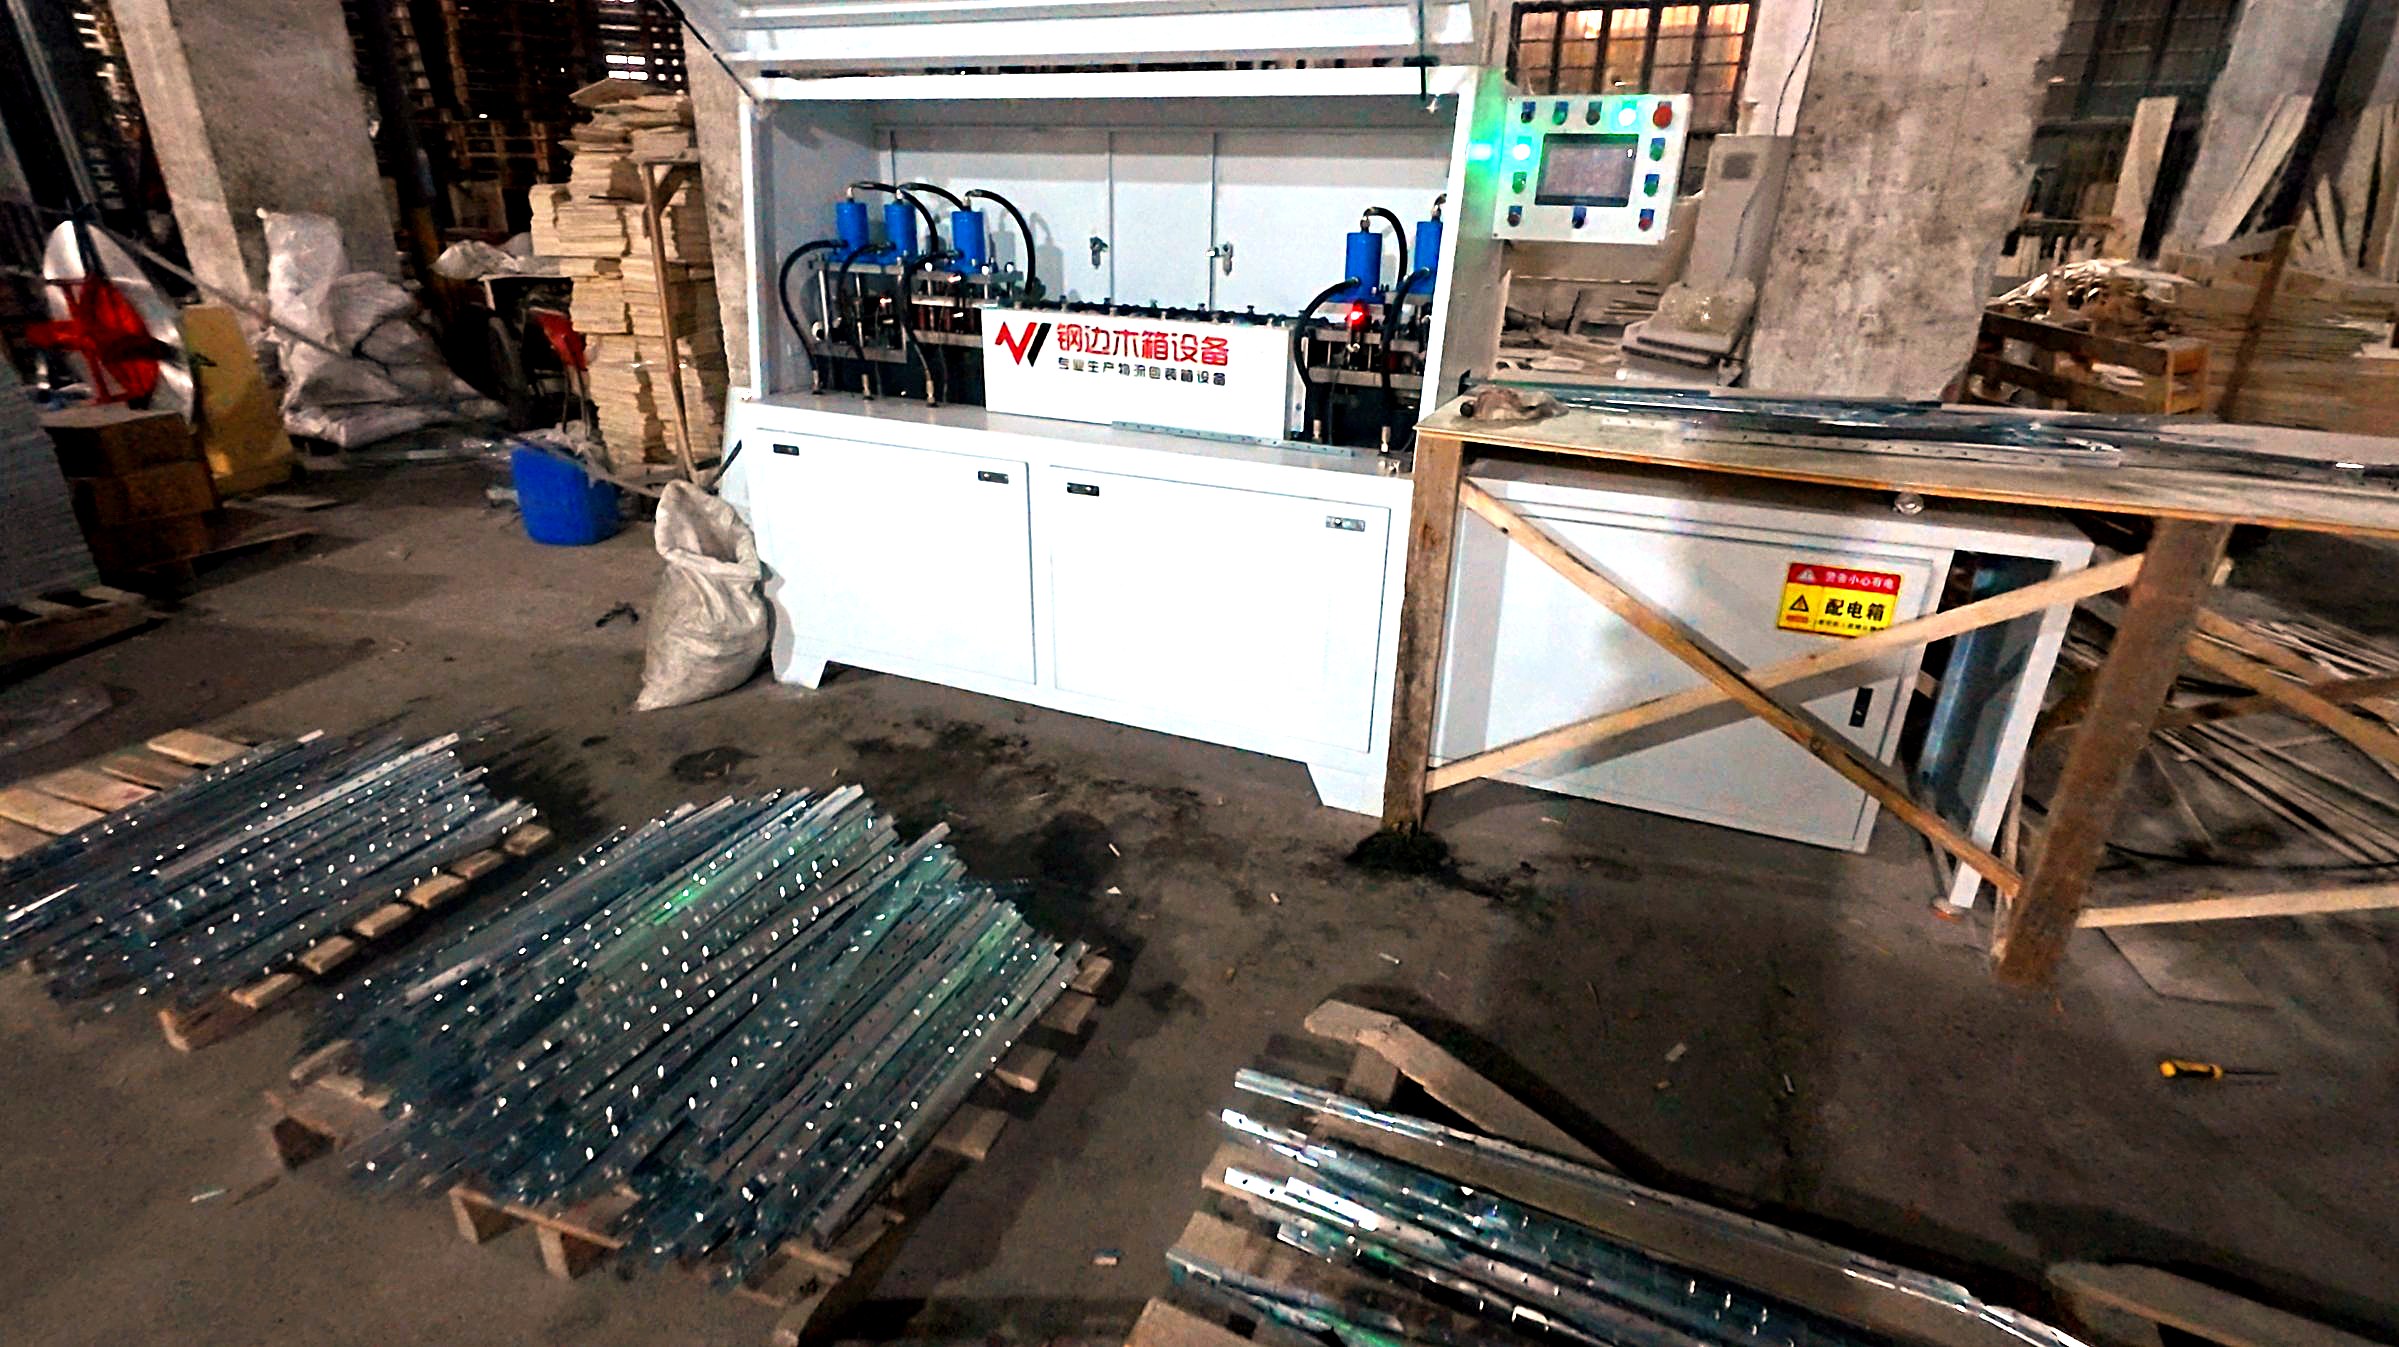
Standard configuration data. Machines are configured to order — contact us for values matched to your product.
| Model | GA-8000 (high speed) |
|---|---|
| Motor power | 6 kW |
| Control system | PLC + servo drive |
| Machine size (L×W×H) | 3,100 × 800 × 1,600 mm |
| Recommended working area | 5 × 2 m |
The standard configuration of the GA-8000. Alternative brands and upgraded configurations are available on request.
| Control system | PLC control system | Omron, Japan |
|---|---|---|
| Servo drive & motor | Servo system | Inovance |
| Die assembly | High-end guide-sleeve design | |
| Screws | 304 stainless steel | |
| Springs | Precision die springs | Daido, Japan |
| Electrical components | Low-voltage electrics set | CHINT |
| Proximity switches | Position sensing set | Xinling |
| Dust protection | Full dust-proof design with cover | |
| Included accessories | Feeder and feed rack |
Guides align the coiled strip for stable, continuous delivery.
Multiple roller stations gradually shape the required profile.
The encoder measures length and triggers cutting at the preset value.
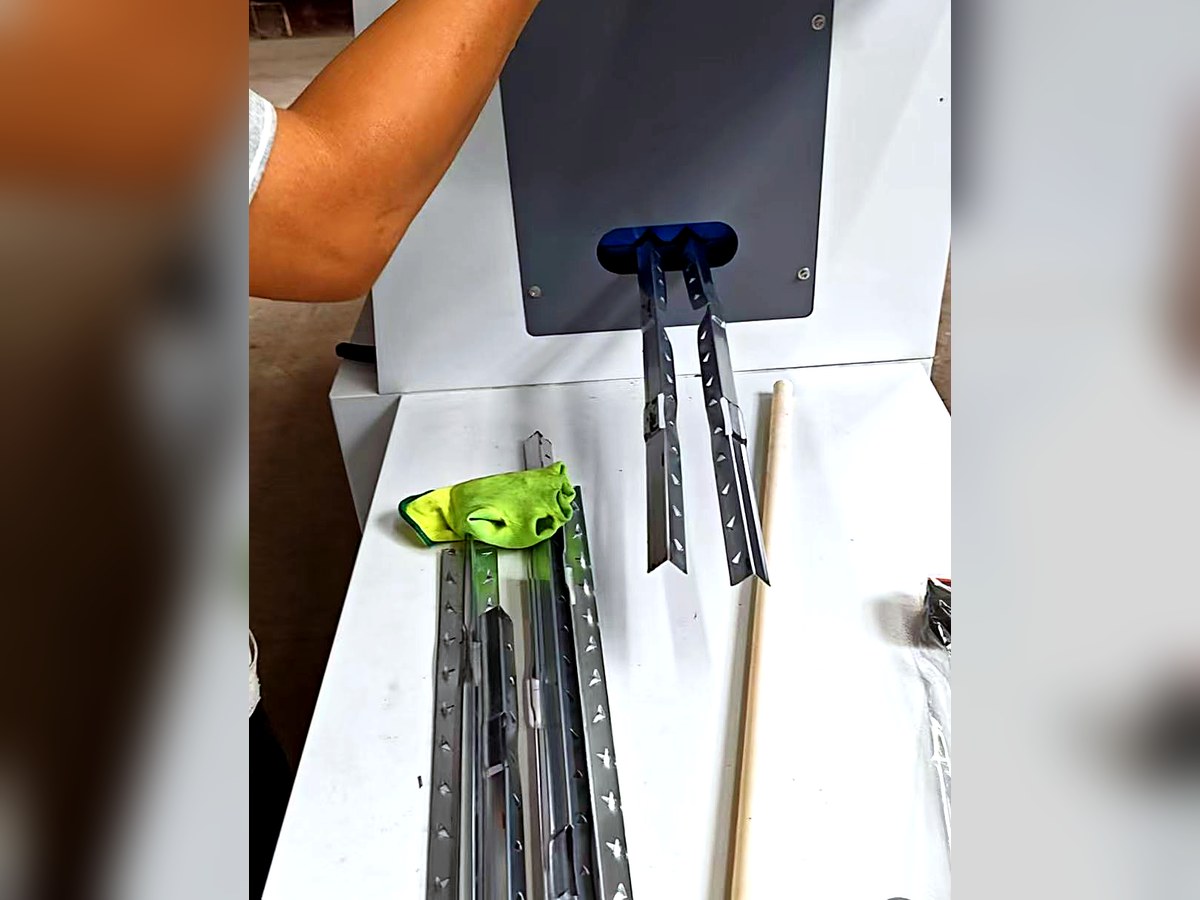
Finished steel edges discharge automatically for downstream pressing.
Inspect guards, chains, bending dies and cutters, and confirm the e-stop and power supply. Run the machine empty for 1–2 minutes and confirm smooth, quiet operation.
Hoist the coil onto the feeder rack and secure it. Thread the strip through the guide wheels, feed rollers and straightening wheels into the bending die.
Enter the edge length on the control panel (e.g. 1200 mm) and confirm the 40 mm strip width and the 90° bend angle for standard L profiles.
Cut 1–2 trial edges and check: length error within ±1 mm, bend angle 90° ±0.5°, clean cuts without burrs. Adjust feed accuracy, die gap and bend depth until qualified.
Switch to automatic: the machine feeds, cuts to length, bends and discharges on its own. Guide the strip lightly by hand — never reach into the die zone — and stack finished edges neatly.
Stop feeding, run empty for 10 seconds to clear remaining strip, then e-stop and power off. Clean iron filings and oil from the table, dies and rollers, and oil the dies against rust.
Safety: wear cut-resistant gloves and keep hands and head out of the feed opening, bending dies, cutters and chains while the machine runs. Stop immediately on noise, jamming, smoke or leakage — never run a faulty machine.