Automatic feeding
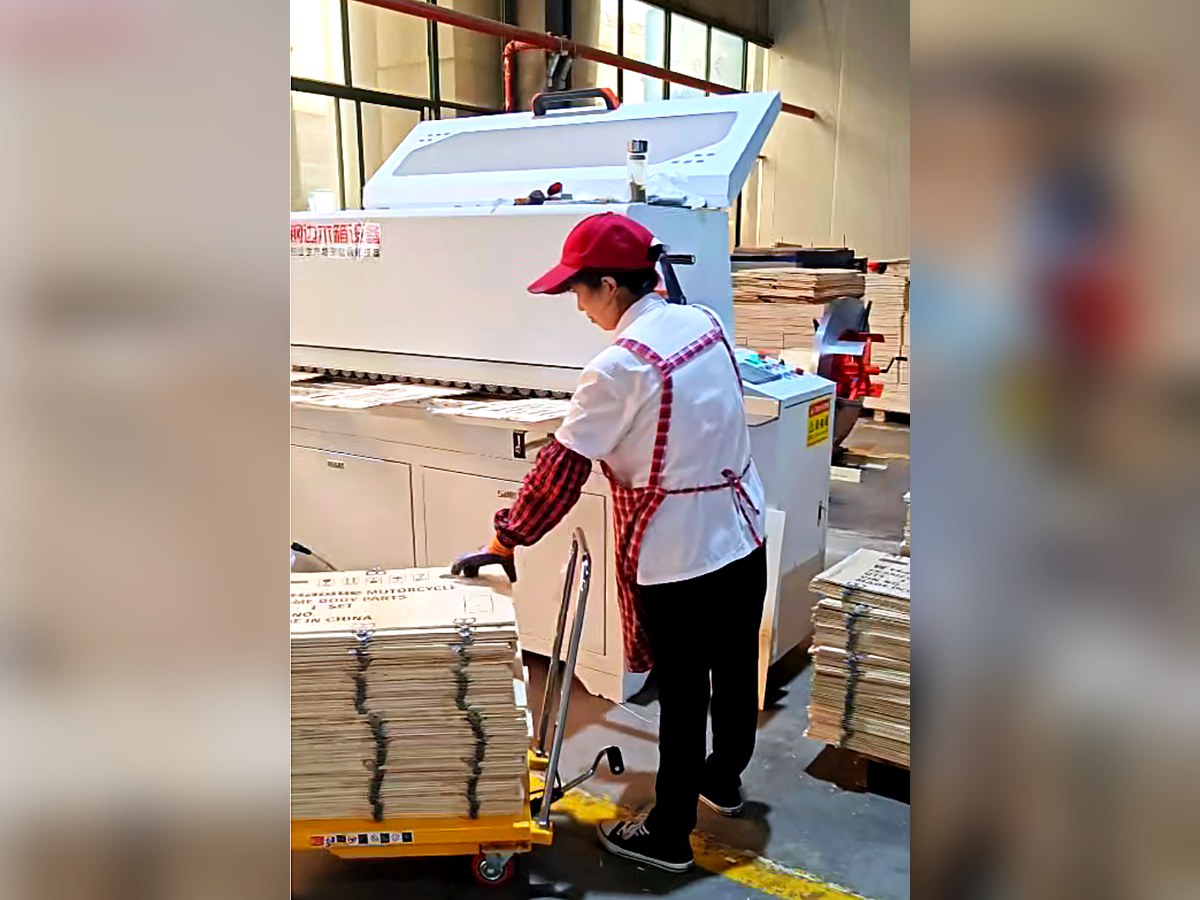
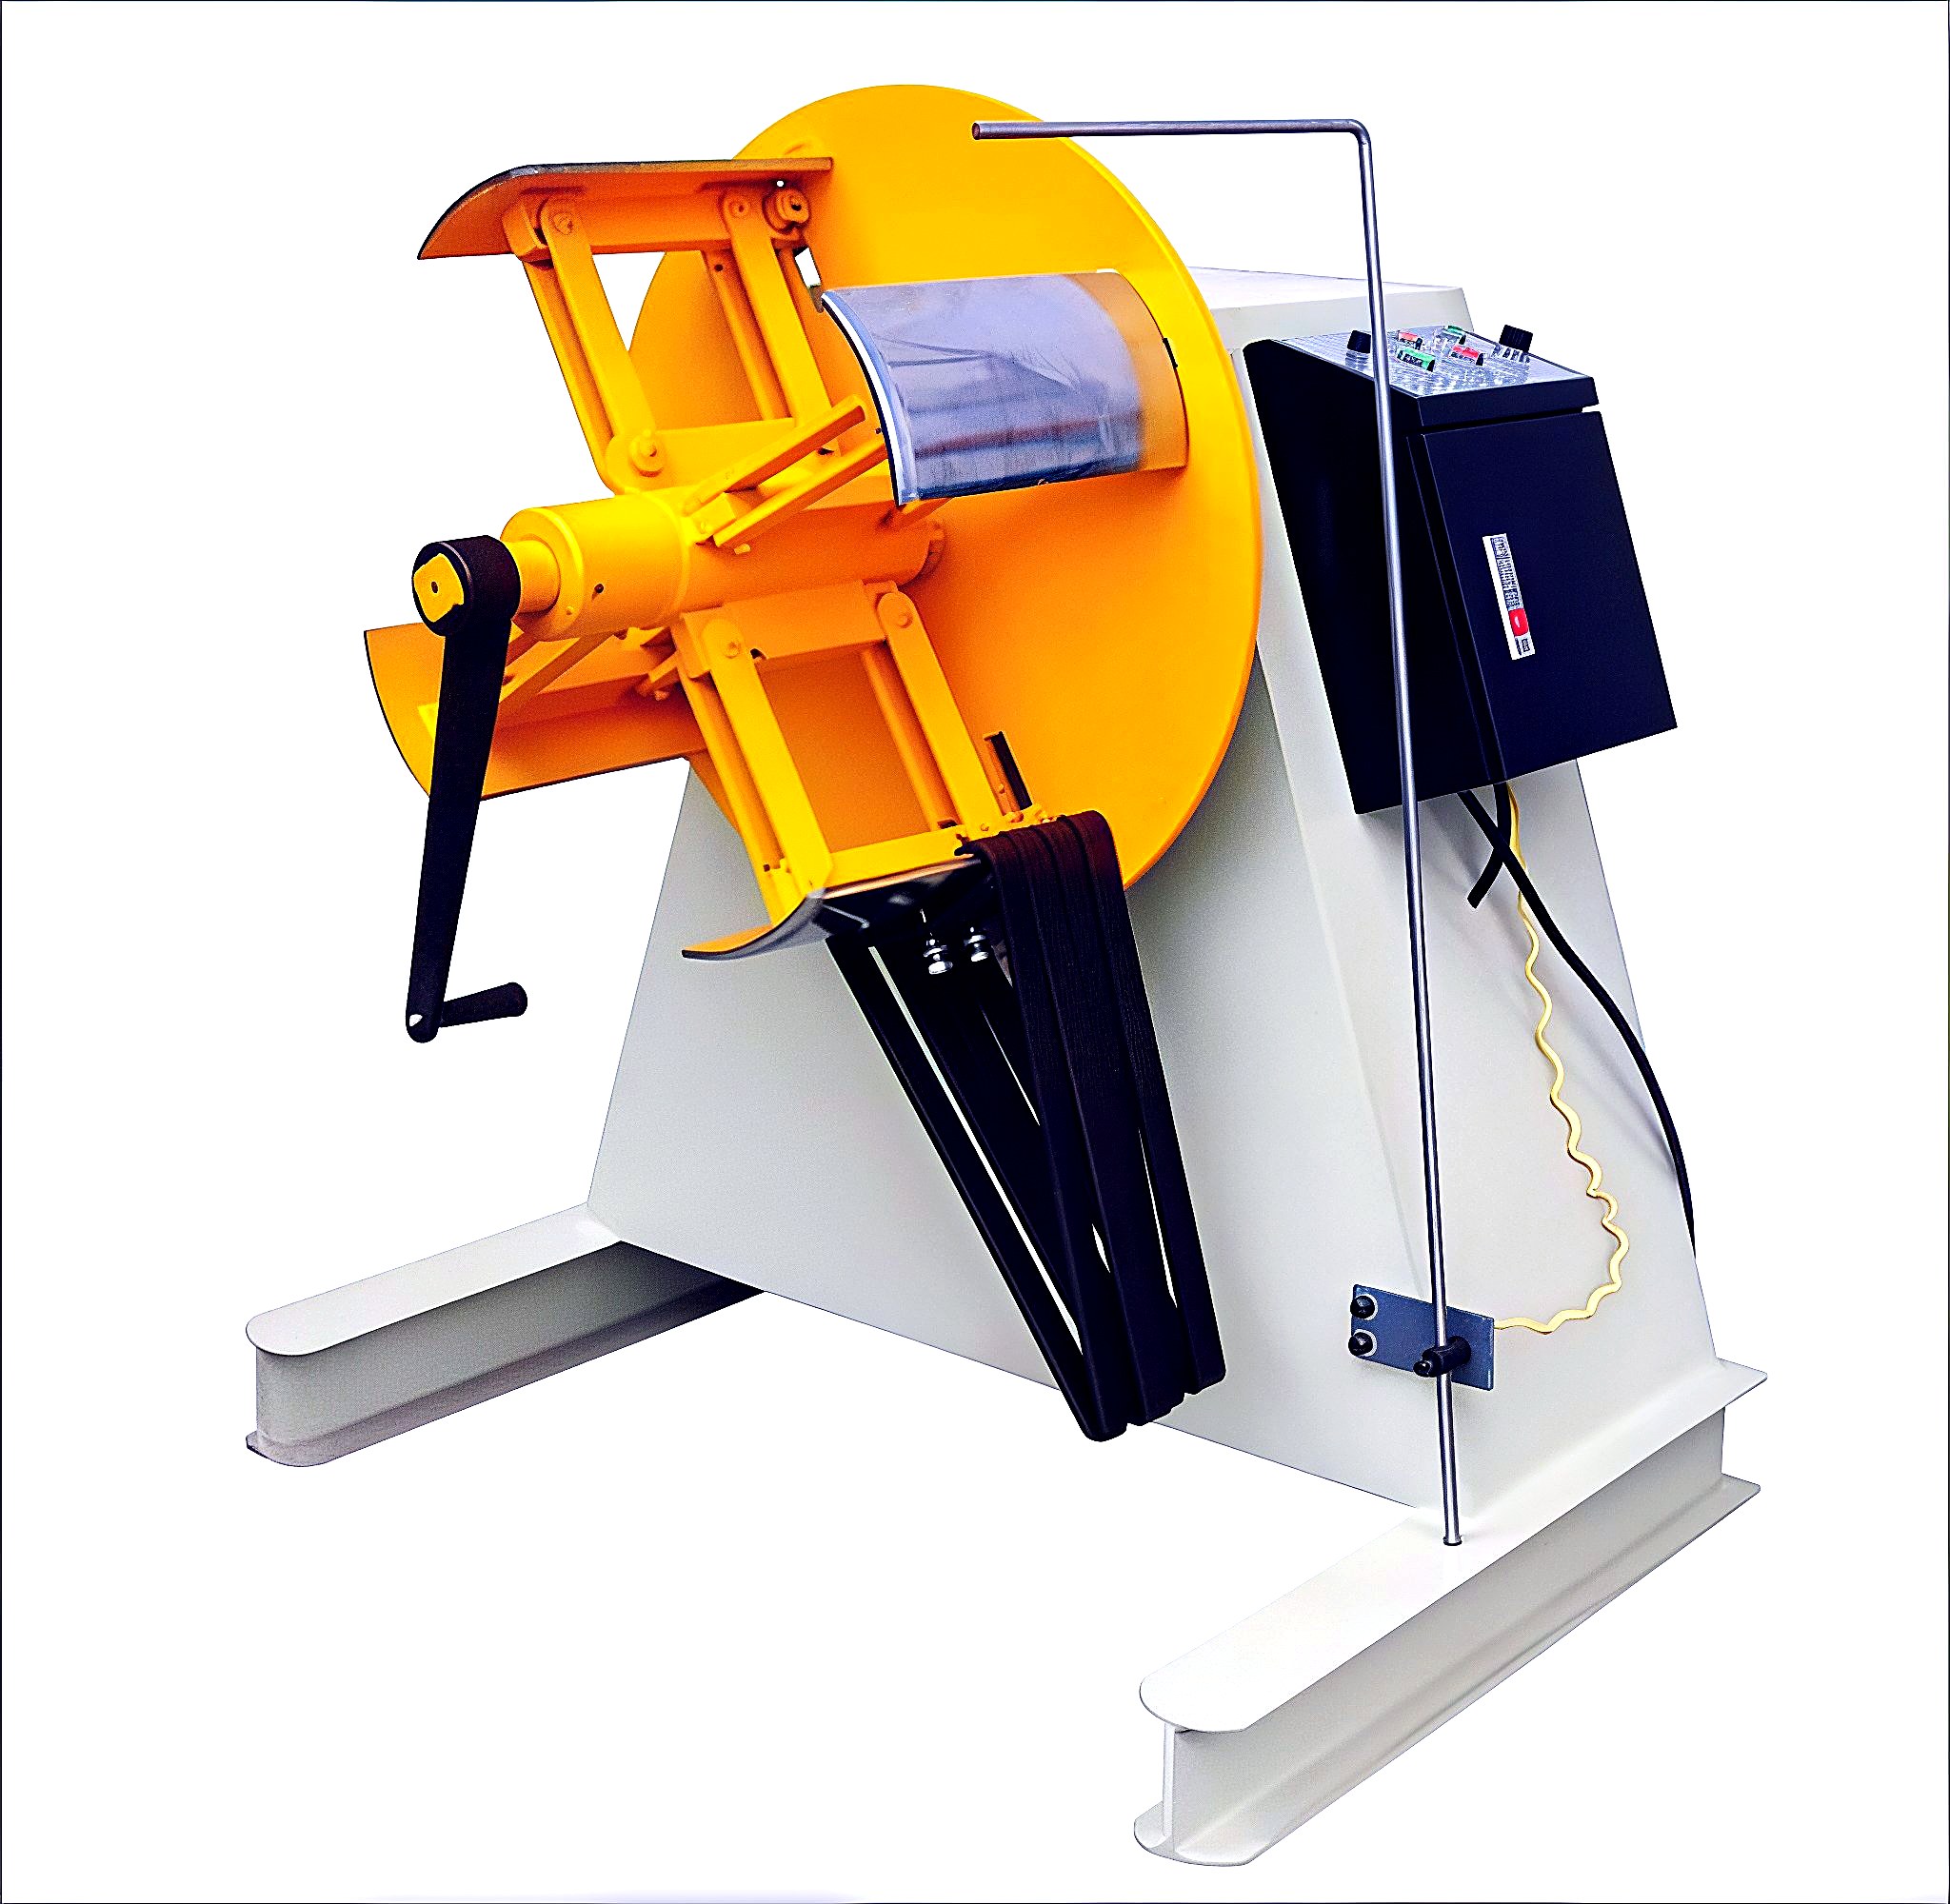
Galvanized steel strip is delivered to the specified position by the feeder.
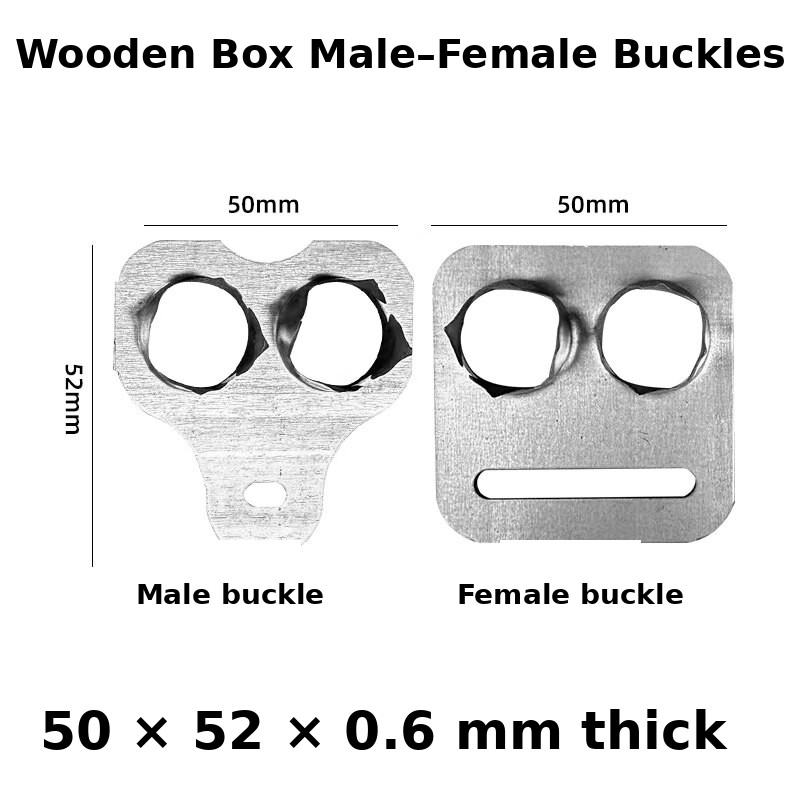
Built on the DA-8000 buckle machine platform with an added female-buckle die and hydraulic cylinder, producing matched male and female buckles for nailless plywood boxes.
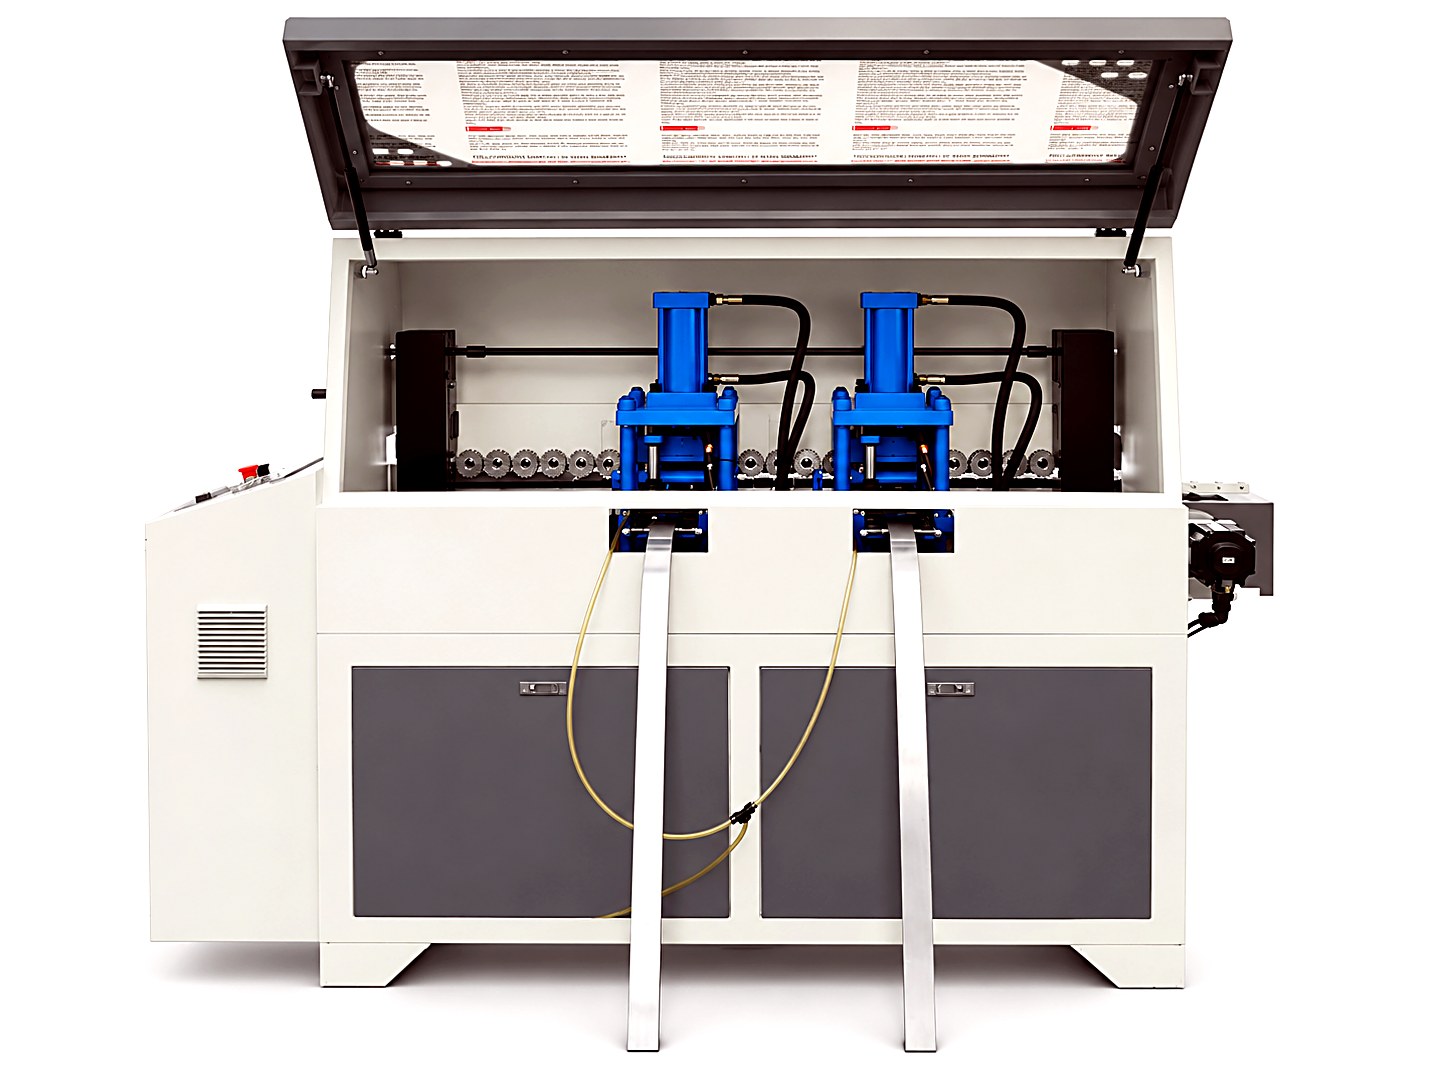
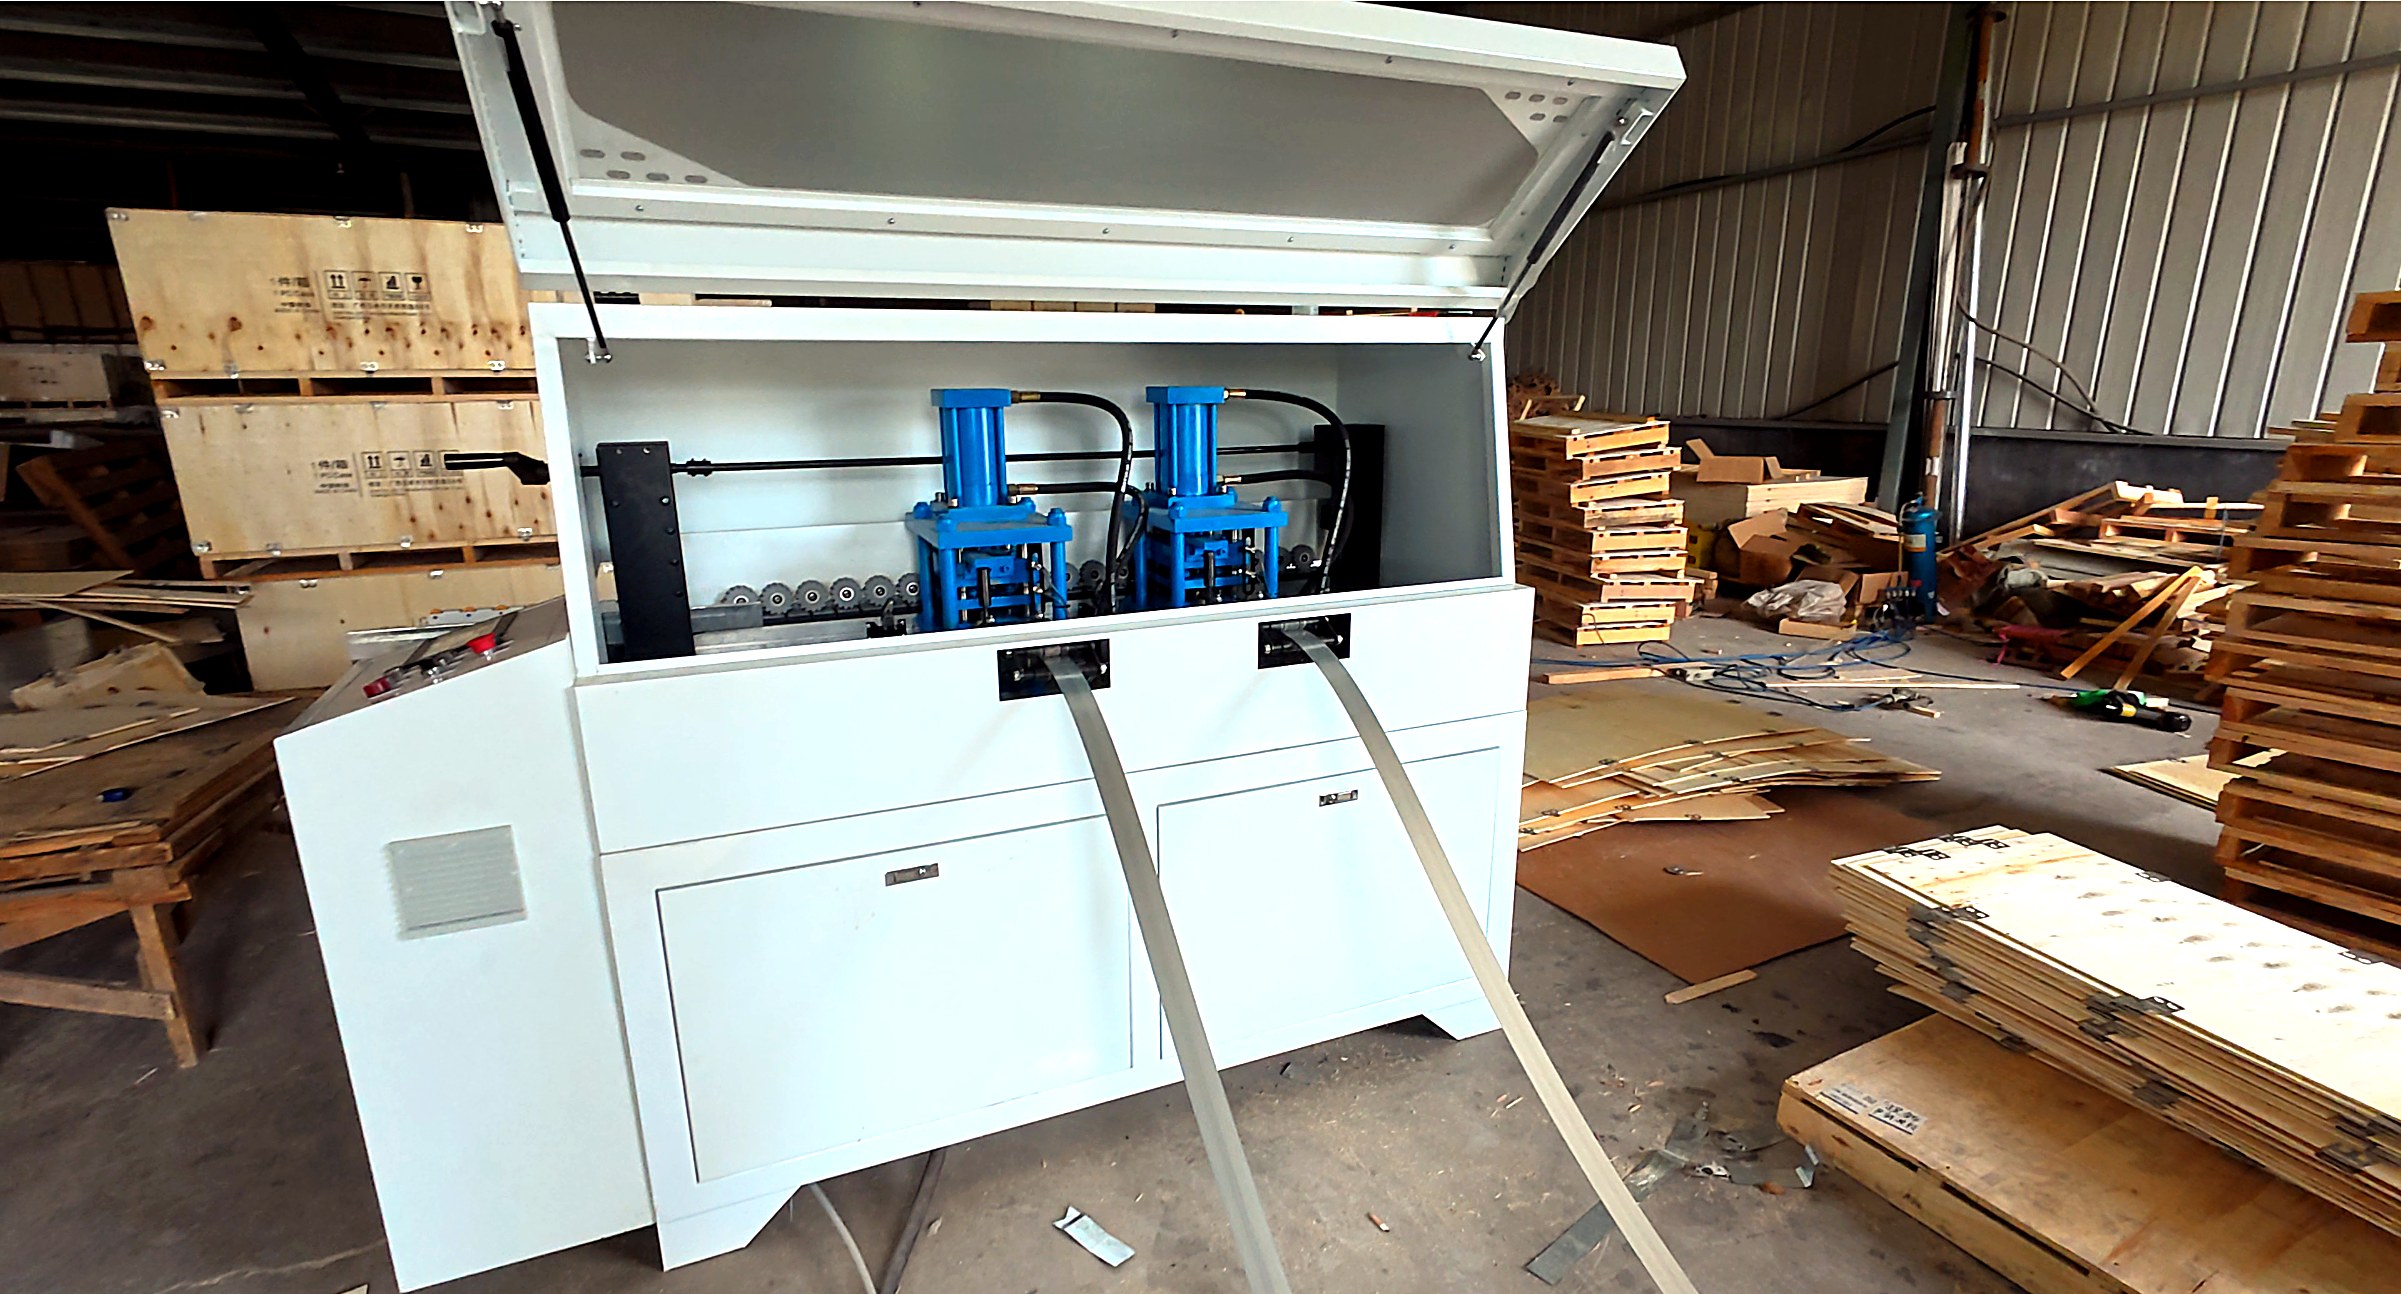
This variant shares the DA-8000 platform — Siemens PLC control, Inovance servo drive, 6 kW drive and 30–60 fastenings per minute — and adds a female-buckle die with an additional hydraulic cylinder. One machine therefore produces both halves of the clasp set: male buckles and female buckles, in the same 50 mm strip and 5–12 mm panel range. The standard DA-8000 produces male buckles only; choose this variant when the box design needs the full male–female fastening set from a single machine. Two automatic steel strip decoilers are included as standard — one per die station.
One machine produces both male and female buckles
Same DA-8000 platform: Siemens PLC + servo positioning, 30–60 fastenings per minute
Additional female-buckle die and hydraulic cylinder included
Matched clasp sets improve box assembly fit and reuse life
Adapts to different panel thicknesses (5–12 mm) and fastener specifications
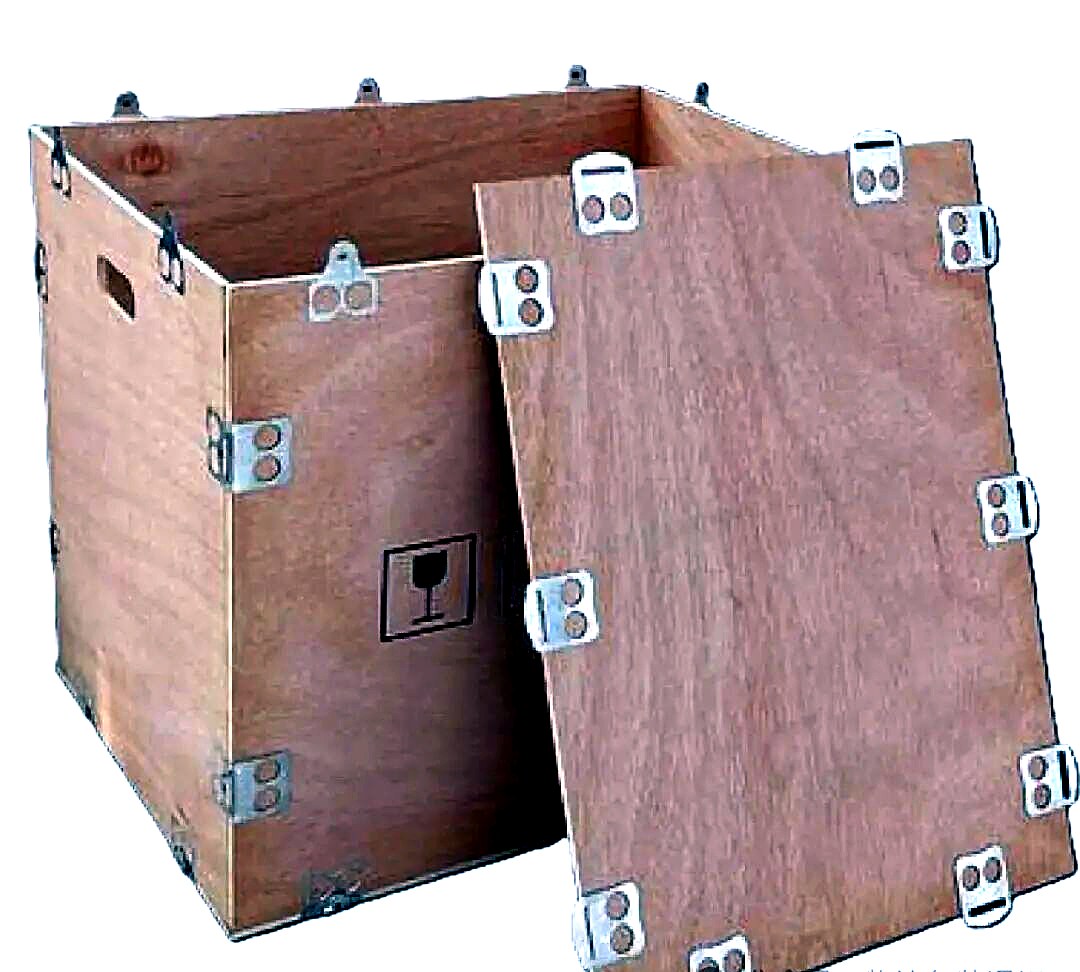
Nailless plywood boxes
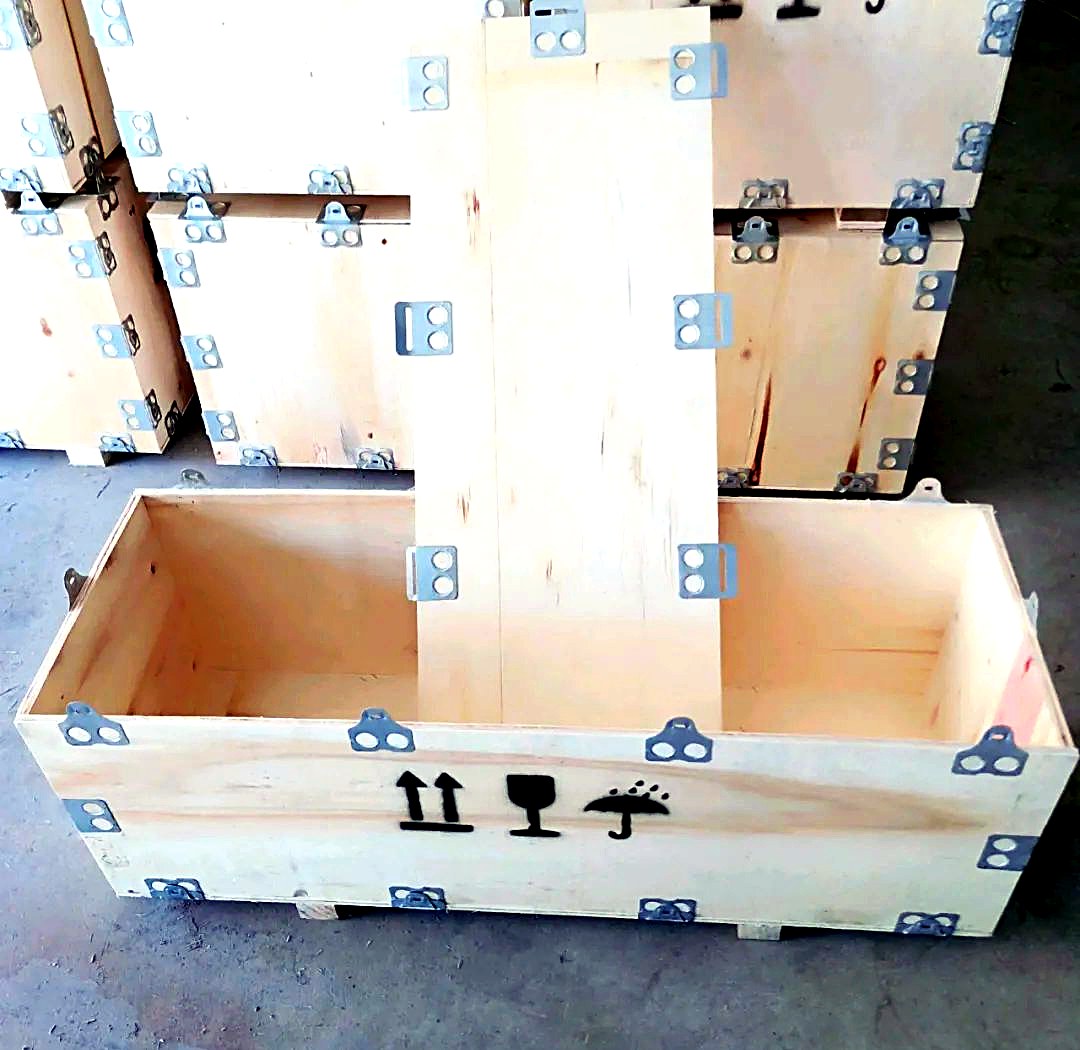
Collapsible wooden boxes
Steel-edged export cases
Reusable industrial transport boxes
Buckle boxes with male–female clasps
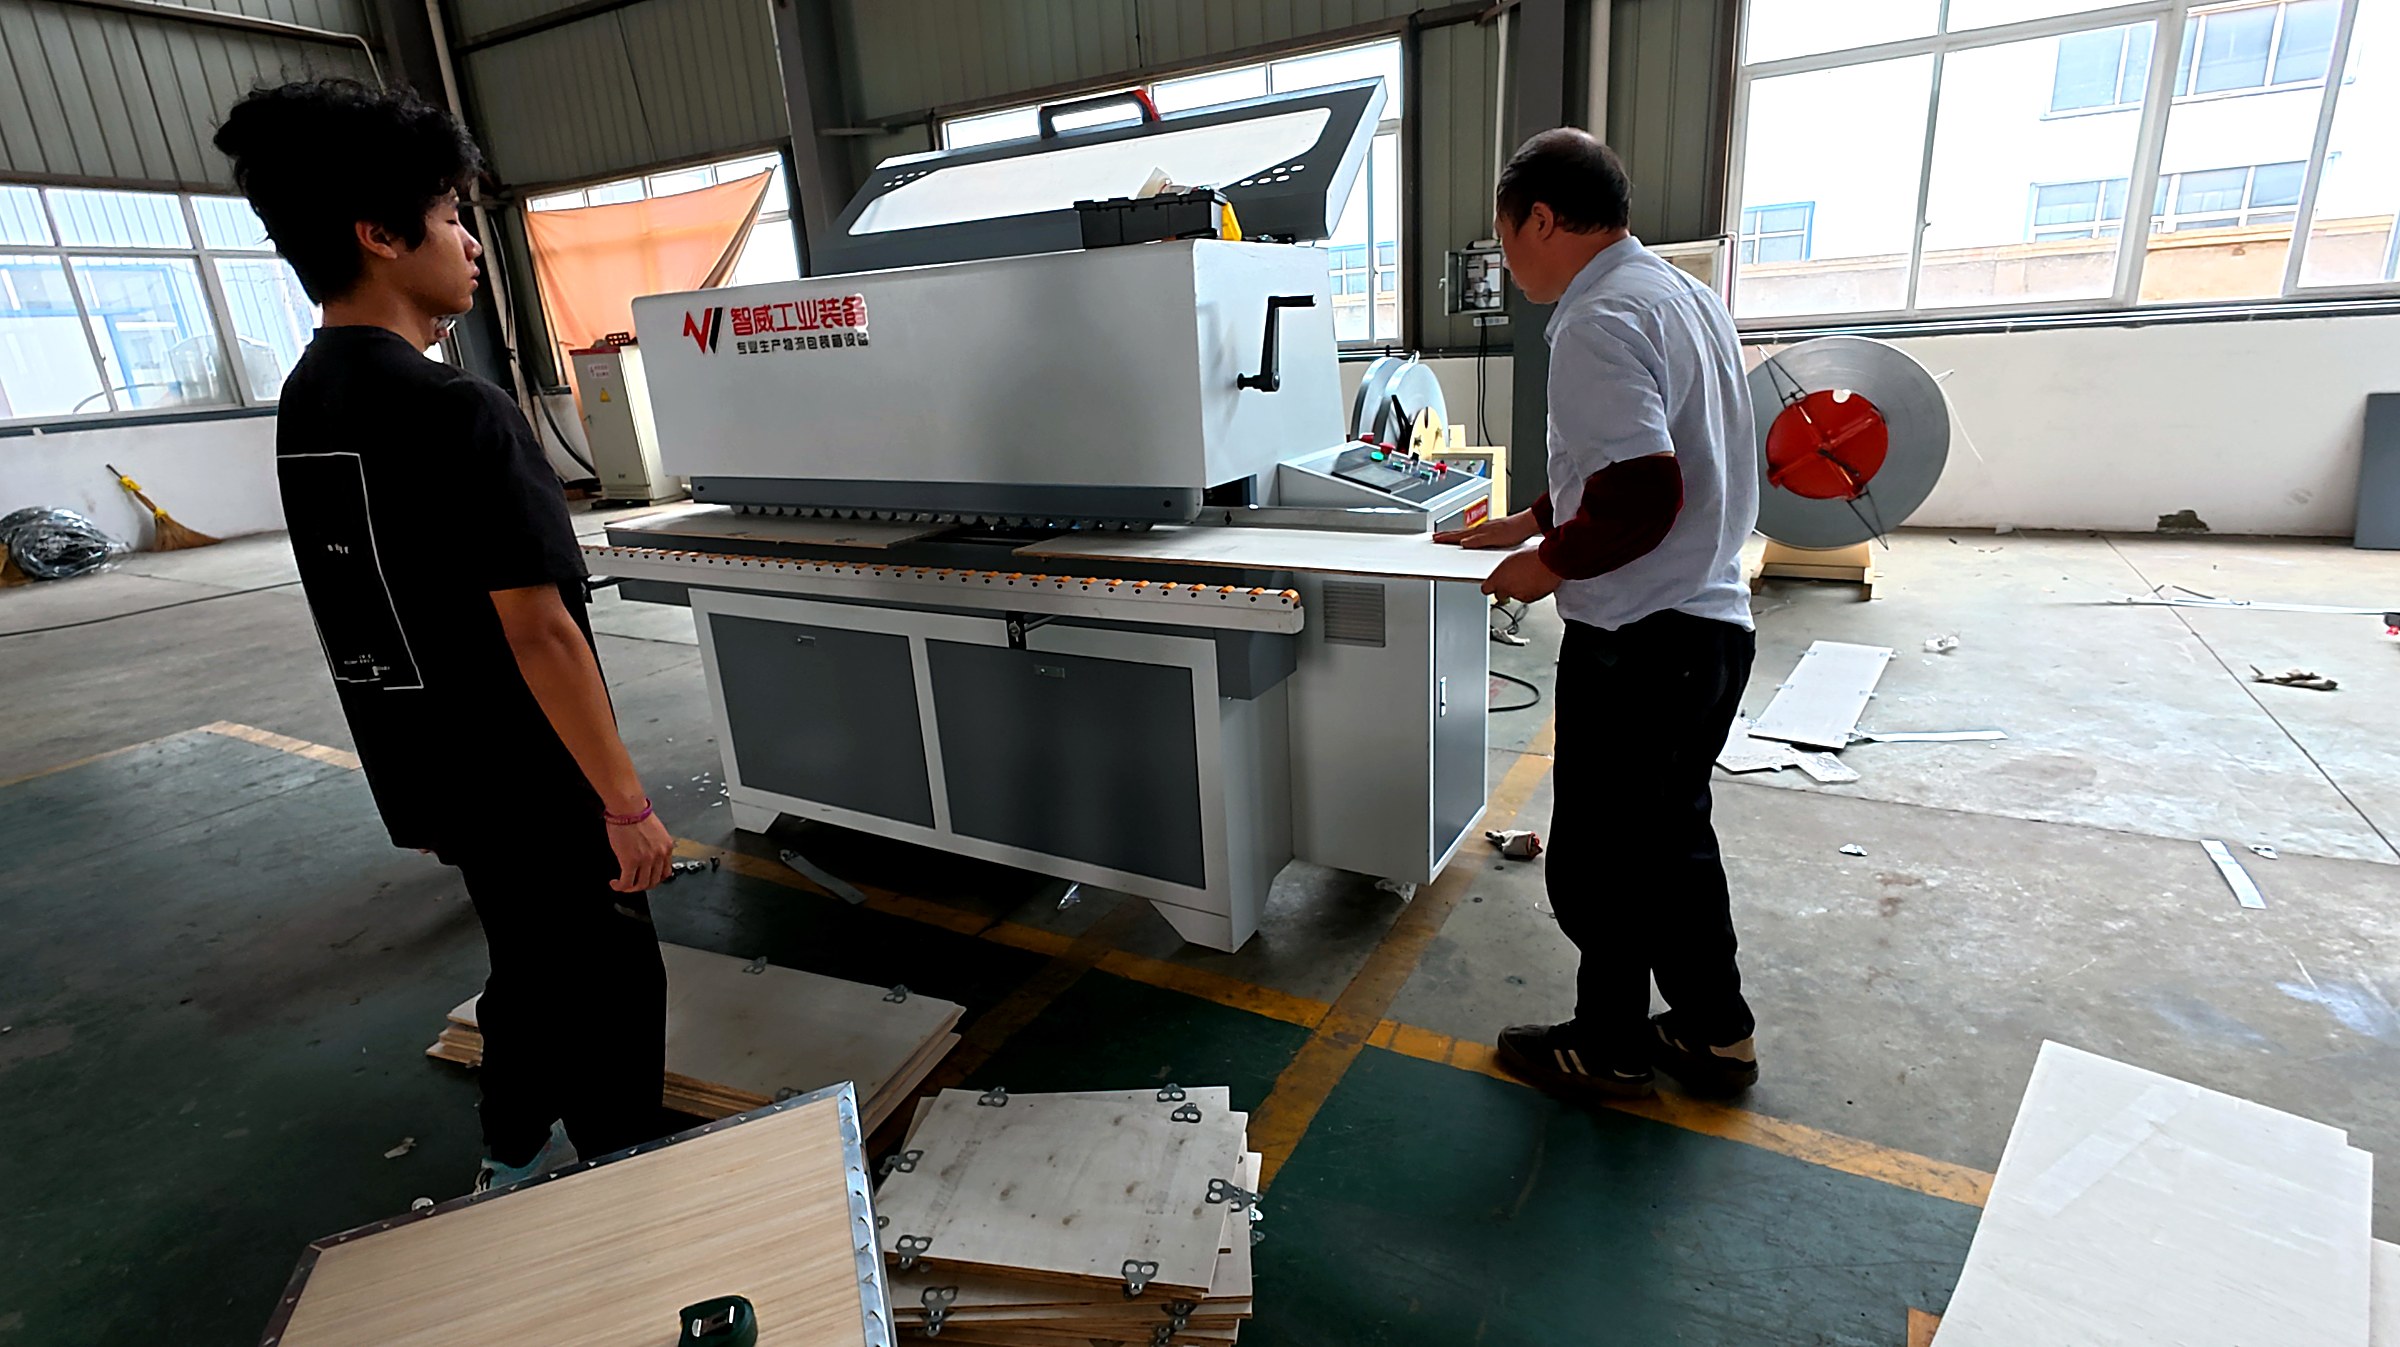
Standard configuration data. Machines are configured to order — contact us for values matched to your product.
| Model | DA-8000 series (male–female type) |
|---|---|
| Motor power | 6 kW |
| Fastening speed | 30–60 /min |
| Applicable steel strip width | 50 mm |
| Applicable panel thickness | 5–12 mm |
| Max. assembly length | 9,000 mm |
| Machine size (L×W×H) | 2,450 × 800 × 1,600 mm |
| Machine weight | 1,000 kg |
| Recommended working area | 3 × 3 m |
| Output | Male buckles + female buckles |
The standard configuration of the DA-8000 series. Alternative brands and upgraded configurations are available on request.
| Control system | PLC control system | Siemens, Germany |
|---|---|---|
| Servo drive & motor | Servo system | Inovance |
| Planetary reducer | Precision planetary reducer | Zhongda Leader |
| Hydraulic die assembly | 120 kg, triple-enlarged outlet design | |
| Female-buckle die | Additional die set for female buckles | |
| Hydraulic cylinder | Additional cylinder for female-buckle forming | |
| Bearings & screws | 304 stainless steel | |
| Springs | Precision die springs | Daido, Japan |
| Electrical components | Low-voltage electrics set | CHINT |
| Proximity switches | Position sensing set | Xinling |
| Dust protection | Full dust-proof design with cover | |
| Included accessories | 2 × automatic steel strip decoilers + feed rack |
Galvanized steel strip is delivered to the specified position by the feeder.
The panel is clamped and aligned accurately with the die.
Male and female buckles are formed and fastened in sequence by the two die stations.
The punches reset and the workpiece advances to the next cycle.
Inspect guards, chains, dies and feed tracks, and match the male and female dies to the buckle set. Run the machine empty for 1–2 minutes and confirm smooth, quiet operation.
Place the matched steel strip in the dies with the correct orientation. Keep both feed tracks clear — no stacking, no jammed buckles.
Lay the plywood panel flat on the worktable and align the fastening point with the center of the die. Hold the panel steady so it cannot shift.
Press start: the two die stations form and fasten the male buckle and the female buckle in sequence, then reset automatically.
Move the box through each fastening point at a steady pace. Check every clasp: buckles flat, tight and matched, with no cracks or dents in the panel.
Run the machine empty for 10–20 seconds to clear the tracks, then stop and power off. Clean the table, tracks and dies, and record the run.
Safety: keep hands out of the pressing, feeding and transmission zones while the machine runs. Stop immediately on jamming, unusual noise or a mis-fastened buckle — never run a faulty machine.